Tested before it is coated. Every valve.
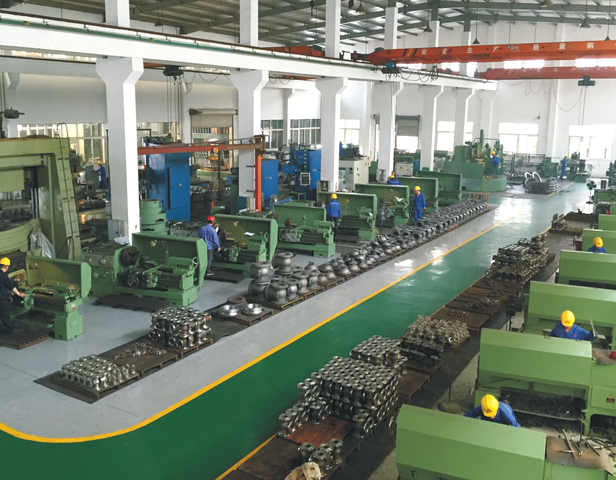
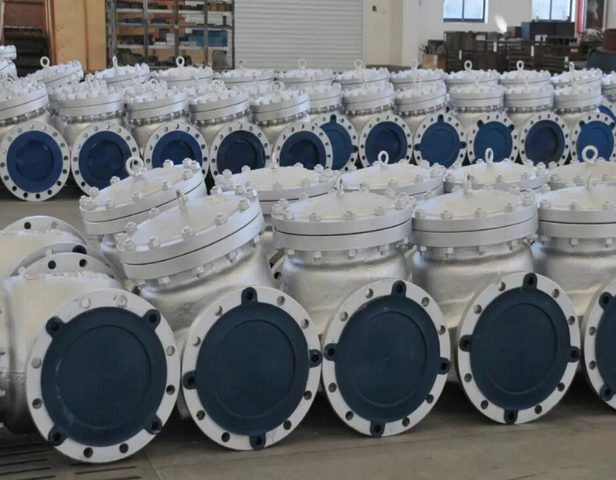
Bodies, balls and stems are machined on CNC centres in Yongjia, then welded, assembled and hydro-tested before coating. The workshop in these photos is the one that builds your order.
CNC Machining
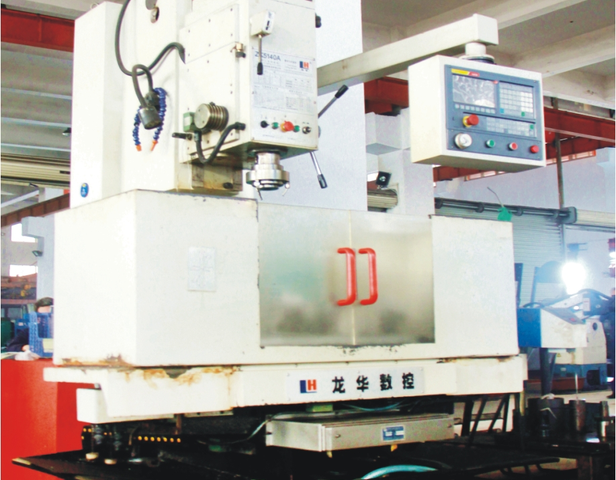
Bodies, balls and stems are machined in-house on CNC centres in Yongjia. Machining the ball and seat faces on the same centres that hold the body is what keeps the sealing geometry concentric.
Pressure Testing
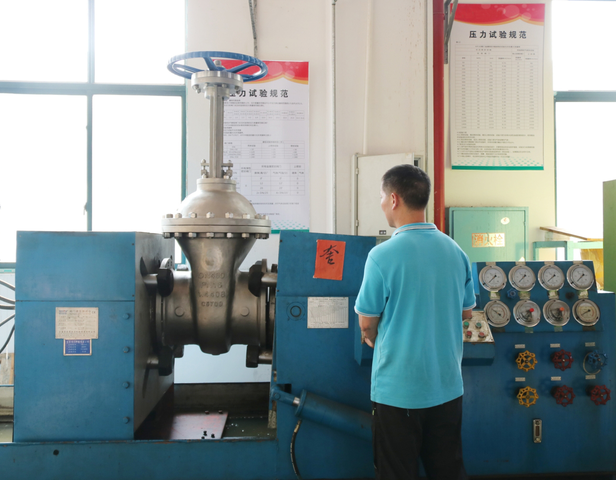
Every valve is shell- and seat-tested to EN 12266-1 before coating — not sampled. Coating goes on only after the test passes, so we are not coating over a defect.
Heat Traceability
Each valve carries a heat number matched to its test record, and the test report ships with the order. That is the document your inspector asks for.
In-House Assembly
Welding, assembly and 3PE or epoxy coating are finished on site. Nothing critical is sub-contracted out from under our own inspection.
Where it is built
What ships with the order
Documents are issued per order rather than kept as a standing wall of logos — tell us what your inspector needs and we will confirm what we can issue.